Project Brief
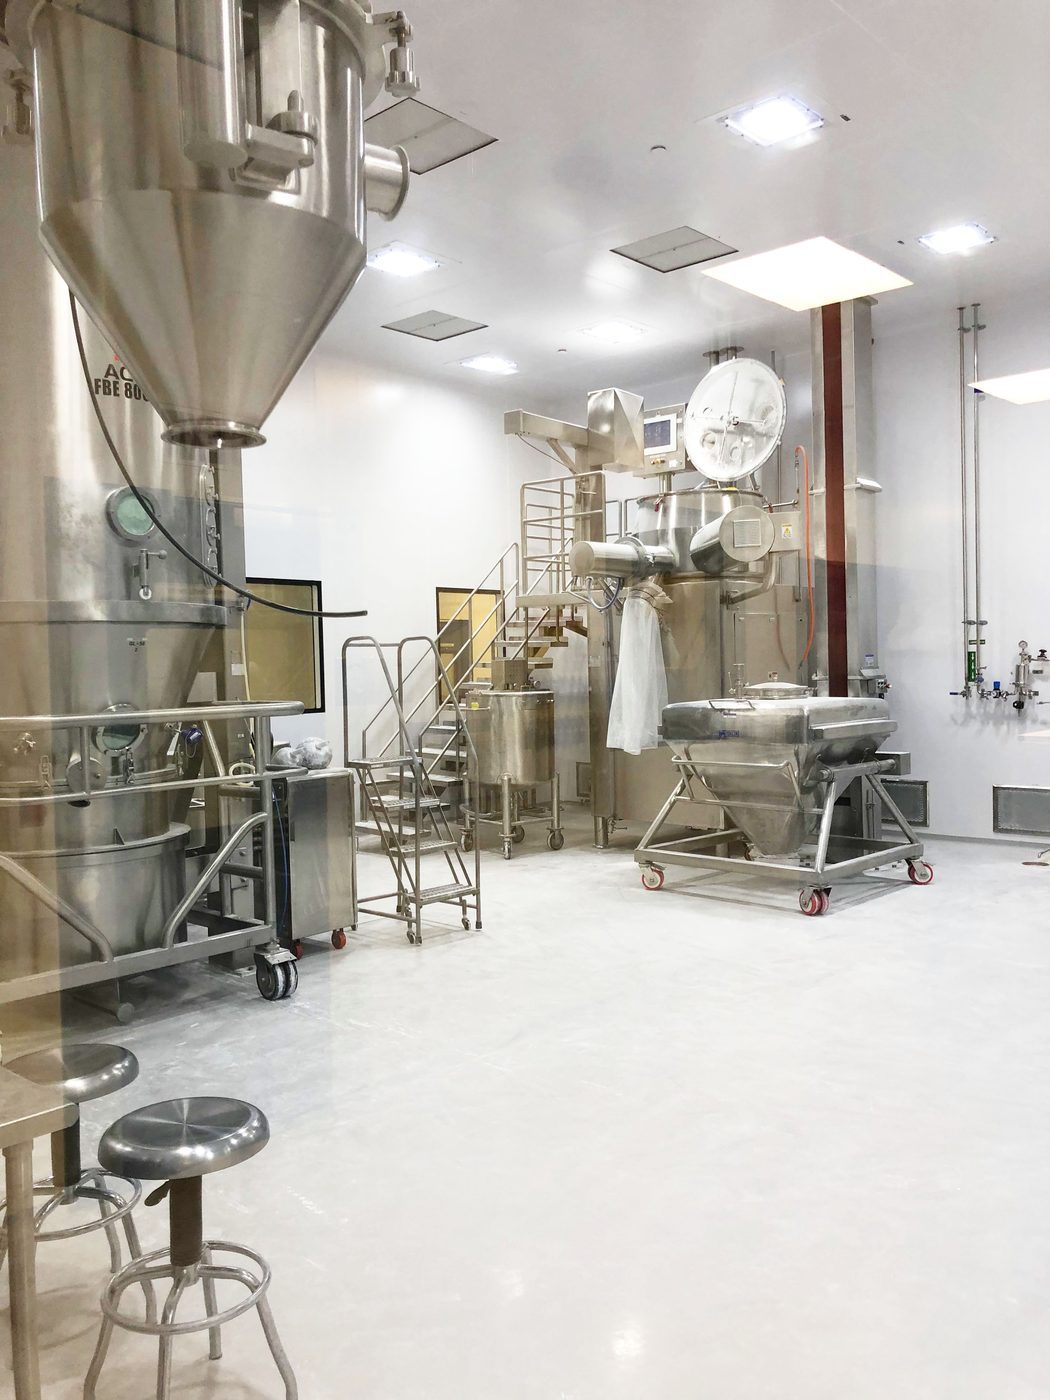
KeRi engineered the mechanical, electrical, plumbing, fire protection and process utility systems for a new high speed triple combi sterile injectable fill-finish line, added as a phase inside an existing pharmaceutical facility alongside the triple combi and vial lines already in production. The suites are classified Grade B and Grade C, with product exposure inside Grade A isolators. Nine air handling units move about 155,000 CFM of supply air and 7,825 CFM of outside air, sized room by room from air change rate and pressure relationship. Classified rooms are served by 99.99% terminal HEPA units, gel-sealed and bottom-loading for room-side filter change and aerosol challenge, with low level return grilles and a pressure cascade holding air from cleaner to less clean. Relative humidity was set at not more than 60%, which the chilled water coils reach without active desiccant dehumidification.
Central plant capacity is 703 tons: two 325 ton air-cooled screw chillers and a 53 ton scroll machine on 30% propylene glycol, with three 750 GPM pumps on variable frequency drives, two lead and one standby. Three 80 BHP natural gas boilers deliver 2,760 lb/hr each at 70 psi, skid mounted with feedwater, condensate, chemical treatment, blowdown separation and a 150,000 grain softener, feeding a 3,722 MBH steam to hot water converter. Process cooling is kept separate from building cooling: a 20 ton water-cooled glycol chiller at 35°F with a 220 gallon stainless buffer tank, plus 2,635 MBH and 723 MBH plate and frame exchangers.
The high purity water train runs from a multimedia filter, activated carbon filter and duplex softener through the pure water generation unit and polisher to a WFI generator, storage tank and distribution skid serving the filling lines, washers, autoclaves and lyophilizer, with pure steam generators for sterilization. Compressed air is three oil-less compressors at 461, 205 and 205 SCFM against 688 CFM demand, an 855 SCFM zero-purge desiccant dryer at minus 100°F pressure dew point and a 1,550 gallon receiver, distributed in welded 316L to ISO 8573-1 Class 1.1.1. Nitrogen runs about 243 CFM at peak from ultra high purity liquid cylinders on an automatic switchover manifold, with vacuum, helium, hydrogen, DI and RO water as separate systems.
Process waste and process vent were kept off the sanitary system, acid waste and acid vent run in polypropylene with fusion-lock fittings, and solvent and toxic waste is collected at the point of use for owner disposal under EPA guidelines. The existing 4,000 A, 277/480 V service was reused: the nine air handling units draw 1,450 A and the three chillers 1,486 A, fed through two new 800 A distribution panels, six mechanical panels and twelve transformers totaling about 695 kVA, including a 20 kVA unit stepping 480 V to 400 V for European process equipment. A 75 kW UPS backs process instrumentation, and three existing 500 kW generators carry 1.5 MW of standby through a 2,500 A transfer switch with shunt-trip load shedding. Fire protection is a new automatic wet sprinkler system by performance specification.
MEP Engineering Scope
What We Engineered
MEP/FP and process utility systems for the high speed triple combi line:
- Grade B and Grade C cleanroom HVAC with Grade A isolators: nine air handling units, about 155,000 CFM supply and 7,825 CFM outside air, with room-by-room pressure cascade
- 99.99% terminal HEPA units, gel-sealed and bottom-loading with room-side aerosol challenge ports, and low level return grilles in the classified rooms
- 703 tons of cooling: two 325 ton air-cooled screw chillers and one 53 ton scroll chiller on 30% propylene glycol, with three 750 GPM primary pumps on VFDs
- 240 BHP steam plant: three 80 BHP natural gas boilers at 2,760 lb/hr and 70 psi, with feedwater, condensate return, blowdown separator, chemical feed, flash tanks and water softener
- 3,722 MBH steam to hot water converter and 190 GPM hot water distribution
- Process cooling separated from building cooling: 20 ton water-cooled glycol chiller at 35°F with 220 gallon stainless buffer tank, plus 2,635 MBH and 723 MBH plate and frame exchangers
- Water pretreatment train: multimedia filter, activated carbon filter and duplex water softener ahead of the pure water generation unit and polisher
- WFI generation, WFI storage tank and WFI distribution skid serving the filling lines, washers, autoclaves and lyophilizer, with pure steam generation for sterilization
- Compressed air: three oil-less compressors at 461, 205 and 205 SCFM against 688 CFM demand, an 855 SCFM zero-purge desiccant dryer at minus 100°F pressure dew point, filtration and a 1,550 gallon receiver, distributed in welded 316L to ISO 8573-1 Class 1.1.1
- Nitrogen at about 243 CFM peak from ultra high purity liquid cylinders on an automatic switchover manifold, plus vacuum, helium, hydrogen, DI and RO water distribution
- Segregated process waste and process vent, acid waste and acid vent in polypropylene with fusion-lock fittings, blowdown separation and condensate neutralization, with solvent and toxic waste collected at the point of use for owner disposal under EPA guidelines
- Electrical reusing the existing 4,000 A, 277/480 V service: two 800 A distribution panels, six mechanical panels, twelve transformers totaling about 695 kVA including a 480 to 400 V unit for European process equipment
- 75 kW UPS for process instrumentation and controls, 1.5 MW of existing standby generation through a 2,500 A transfer switch, and shunt-trip load shedding on five existing panels
- New automatic wet sprinkler system by performance specification, fire alarm, and BMS controls monitoring the classified rooms
The Challenge
A new high speed sterile injectable line had to be built into a live facility, hold Grade B and Grade C conditions with Grade A isolators, and share central utilities with the triple combi and vial lines already running, without a new electrical service.
Our Solution
KeRi sized the air, water, steam, gas and waste systems for the combined load rather than the new line alone: nine air handling units with 99.99% terminal HEPA on a pressure cascade, 703 tons of cooling and a 240 BHP steam plant, a full pretreatment and WFI train with pure steam, compressed air and nitrogen in welded 316L, segregated process and acid waste, and a distribution redesign that reused the existing 4,000 A service and 1.5 MW of standby generation.
Previous Project Aseptic Fill-Finish Facility Next Project Aseptic BFS Facility